Inquiry
Form loading...

How to Choose DIN Bellows Sealed Gate Valves in 2026?

Choosing Din Bellows Sealed Gate Valves in 2026 requires more than comparing pressure ratings and purchase prices. The correct choice protects process media, reduces fugitive emissions, and supports safer maintenance. Valve industry educator Greg Johnson offers a practical reminder: “A valve must be selected for the application, not merely the line size.” That principle remains valuable when reviewing modern DIN standards, materials, and operating conditions.

The selection should begin with the actual service. Record the medium, temperature, pressure, flow direction, cycle frequency, and available installation space. A stainless-steel bellows may suit corrosive or high-purity duties, while another alloy may perform better in hot chemical service. Check the body rating, end connection, stem design, bonnet construction, and sealing arrangement. Do not overlook actuator compatibility.

Small details matter.

The bellows must tolerate repeated movement without fatigue. The gate should close smoothly, even after long periods without operation. Ask for material certificates, pressure-test records, leakage data, and documented quality procedures. These records do not guarantee perfect field performance. They do improve accountability.

In 2026, buyers should also examine lifecycle cost, spare-part availability, inspection access, and supplier engineering support. A low-cost valve can become expensive when replacement requires shutdown delays. Yet premium pricing alone proves nothing. This is where careful comparison becomes essential.

This guide will explore how to evaluate Din Bellows Sealed Gate Valves for demanding industrial applications. It will also question common assumptions, because catalog descriptions rarely reveal every installation challenge.

How to Choose DIN Bellows Sealed Gate Valves in 2026?

DIN Bellows Sealed Gate Valves: Definition, Design, and Operating Principles

How to Choose DIN Bellows Sealed Gate Valves in 2026?

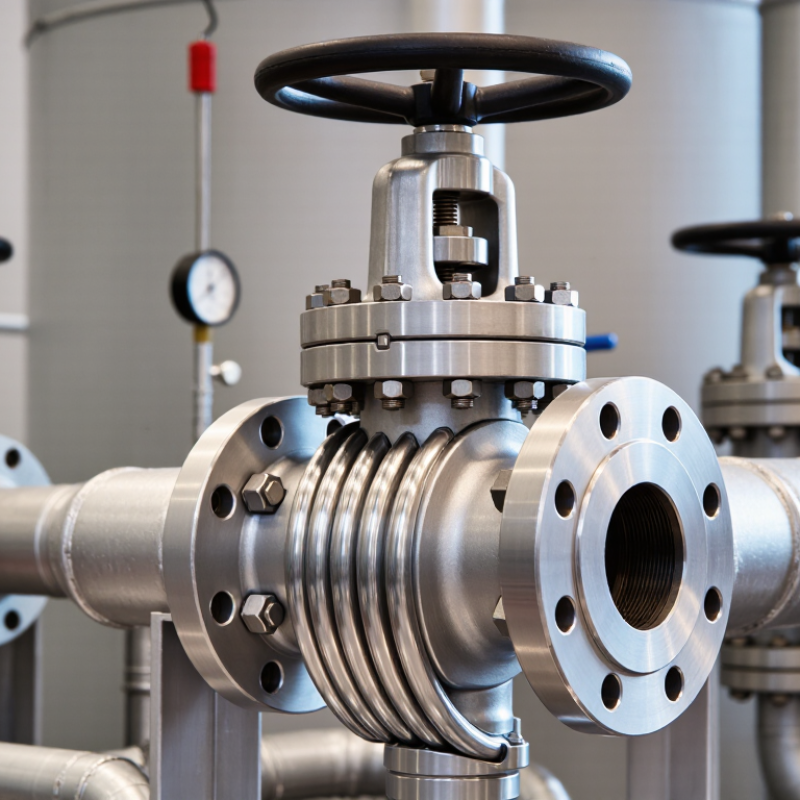
A DIN bellows sealed gate valve controls flow with a rising or non-rising stem and a vertical gate. Its welded metal bellows isolate the stem from the process medium. This design reduces fugitive emissions around the stem packing area. The U.S. Environmental Protection Agency identifies valves as a major source of equipment-leak emissions, reaching about 60% in some petroleum-refining studies. That figure makes sealing design more than a maintenance detail.

Inside the valve, the gate moves away from the flow path when fully open. This creates low pressure loss and supports pipeline isolation. The bellows compress and extend during operation, while the bonnet protects them from external damage. DIN dimensional and pressure requirements help engineers compare compatible valves, but they do not replace application checks. Temperature, pressure, fluid toxicity, corrosion, and cycling frequency must be reviewed together. Small details matter.

For 2026 purchasing, request bellows cycle data, shell-test results, seat-leakage classification, and material certificates. ISO 15848-1 testing is useful for evaluating industrial valve fugitive-emission performance. A thermal-fluid service may need stainless steel bellows, while abrasive service can require stronger gate and seat materials. Do not select only by nominal diameter. That shortcut fails surprisingly often. Field experience also shows that poor alignment, excessive actuator force, and dirty pipelines shorten service life. A valve can meet the specification and still perform badly. Selection should include installation conditions, inspection access, spare-bellows strategy, and documented maintenance intervals.

Identify the Process Requirements and Valve Selection Criteria

How to Choose DIN Bellows Sealed Gate Valves in 2026?

Choosing DIN bellows sealed gate valves in 2026 starts with the process, not the catalog. Define the medium, temperature, pressure, flow direction, and operating frequency. Note whether the line carries steam, corrosive chemicals, toxic fluids, or clean utilities. Bellows sealing reduces external leakage, but it does not correct poor sizing. Record minimum and maximum conditions. Real plants rarely operate at one stable point. This is easy to overlook.

Match the valve body and trim to the medium’s chemistry and temperature. Check pressure class, end dimensions, face-to-face length, and installation space against piping drawings. Forged and cast constructions may suit different pressure and maintenance requirements. Confirm the bellows material, stem design, packing arrangement, and bonnet configuration. For frequent cycling, review fatigue life and actuator compatibility, even when manual operation seems sufficient. Request test records covering shell strength, seat tightness, and bellows integrity. Verify applicable DIN and project standards before approval.

Selection should also consider maintenance access, spare-part availability, emergency isolation, and operator safety. A valve may fit technically yet frustrate technicians beside a crowded pipe rack. Use measured data from similar service where possible. I have seen undersized valves create unnecessary pressure loss and oversized valves complicate operation. That mistake is preventable, but not always obvious during design. Document assumptions in the datasheet, especially uncertain chemistry or transient pressure. Recheck them with operations before ordering. Good engineering includes doubt.

How to Choose DIN Bellows Sealed Gate Valves in 2026? — Identify the Process Requirements and Valve Selection Criteria
Selection Dimension Process Requirement to Identify Typical Selection Data Recommended Valve Criteria Verification Standard or Engineering Check
Valve Type Need for low-emission isolation, positive shut-off, and minimal stem leakage. Rising-stem gate valve with welded or replaceable bellows seal. Use a bellows-sealed gate valve where fugitive-emission control is more important than frequent throttling. Specify the required emission test procedure and acceptance class in the purchase specification.
Applicable Design Standard European/DIN-based project specifications and piping-class requirements. EN 1984 for industrial gate valves is commonly used for design and manufacturing requirements. Request compliance with the project’s stated edition of EN 1984 or the applicable national adoption. Confirm valve design, end connections, materials, testing, and documentation are aligned with the project standard.
Nominal Size Pipe outside diameter, line size, flow area, and available installation space. DN 15 to DN 600 are common industrial sizes; larger sizes require project-specific review. Select the valve DN to match the piping system unless a hydraulic or layout study justifies a reduction or enlargement. Check compatibility with EN 1092-1 flange dimensions, piping tolerances, actuator clearance, and maintenance access.
Pressure Rating Maximum operating pressure, design pressure, pressure surges, and pressure-temperature rating. Typical nominal pressure classes include PN 16, PN 25, PN 40, PN 63, PN 100, and PN 160. Choose a PN rating that exceeds the governing design condition at the actual operating temperature. Do not select by PN value alone; verify the manufacturer’s pressure-temperature rating for the body, bonnet, bellows, and seat materials.
Operating Temperature Normal, minimum, maximum, start-up, shutdown, and upset temperatures. Carbon steel is often used for moderate-temperature service; stainless and alloy steels are selected for corrosion or higher-temperature duties. Ensure the body, stem, bellows, packing, gasket, and seat materials are all suitable for the complete temperature range. Use the lowest design temperature for toughness checks and the highest design temperature for pressure derating.
Process Medium Gas or liquid phase, toxicity, flammability, purity, corrosiveness, solids, and polymerization tendency. Steam, thermal oil, nitrogen, oxygen, hydrocarbons, acids, alkalis, and toxic or volatile fluids may require different materials and cleaning procedures. Confirm chemical compatibility for the body, trim, bellows, seat, gasket, and packing; avoid unverified material substitutions. Review the process safety data sheet, corrosion allowance, oxygen-cleaning requirements, and hazardous-area rules where applicable.
Body Material Pressure, temperature, corrosion environment, and required impact toughness. Common options include carbon steel, austenitic stainless steel, and alloy steel castings or forgings. Use carbon steel for compatible non-corrosive service; select stainless or alloy material when corrosion, temperature, or cleanliness demands it. Require material certificates, normally to EN 10204 type 3.1 or the project’s specified certification level.
Trim and Seat Wear, erosion, corrosion, temperature, tightness, and required cycle frequency. Metal-seated trim is common for high-temperature and fire-risk services; resilient seats may be used when permitted by temperature and medium. Specify gate, seat, stem, and backseat materials separately rather than identifying only the body material. Check seat leakage testing to EN 12266-1 or the project-required test specification.
Bellows Construction Required service life, pressure differential, temperature cycling, vibration, and emission-control target. Multi-ply formed bellows can provide redundancy; welded bellows require careful fatigue and weld-quality control. Request the bellows material, number of plies, design cycle rating, weld inspection, and leakage-test method. Obtain documented bellows fatigue calculations or cycle testing based on the specified operating profile.
Fugitive-Emission Control Regulatory limits or plant targets for stem and bonnet leakage. Low-emission service may require qualification to ISO 15848-1 or an equivalent project specification. Specify the temperature class, mechanical cycle class, leakage rate, test medium, and acceptance criteria. Verify the test certificate applies to the same valve design, stem seal arrangement, and operating temperature range.
End Connection Piping flange standard, pressure class, maintenance strategy, and available space. Flanged ends are widely used; butt-weld ends may be selected for compact or high-integrity piping systems. Match flange facing, drilling, pressure class, and face-to-face dimensions to the piping class. Check EN 1092-1 for flanges and EN 558 for face-to-face dimensions where those standards are specified.
Face-to-Face Dimension Replacement of an existing valve or installation within a fixed piping layout. Dimensions vary by DN, pressure class, valve pattern, and applicable standard. Specify the required series and confirm the valve’s actual certified dimension before fabrication. Use EN 558 or the project’s dimensional standard; do not rely on nominal size alone.
Flow Direction and Installation Horizontal or vertical pipe orientation, drainability, access, and thermal movement. Gate valves are normally used for fully open or fully closed isolation, not continuous throttling. Install according to the valve manufacturer’s orientation limits; provide clearance for handwheel or actuator removal. Confirm bonnet orientation, support loads, insulation clearance, and whether the valve must be installed stem-up.
Actuation Manual operation frequency, operating torque, emergency requirements, and remote control. Handwheel, bevel gear, pneumatic actuator, electric actuator, or hydraulic actuator. Size the actuator for breakaway, running, seating, unseating, and worst-case differential-pressure torque. Define fail position, travel limits, torque switches, position indication, and control-signal requirements.
Fire-Safe Requirement Hydrocarbon, flammable-fluid, or classified process service. Fire-safe qualification may be required for the complete valve assembly. Specify fire testing where required, together with secondary sealing and anti-blowout stem provisions. Reference ISO 10497 or the project’s accepted fire-test standard and request a valid test report.
Pressure and Functional Testing Shell integrity, seat tightness, backseat performance, and operational reliability. Hydrostatic shell and seat tests are typical; pneumatic testing may be used under controlled procedures. Include test pressure, duration, test fluid, allowable leakage, and bellows leakage criteria in the purchase order. Use EN 12266-1 or the project-specified test standard, and require certified test records.
Documentation Traceability, inspection, maintenance, regulatory approval, and turnover requirements. Data sheet, dimensional drawing, material certificates, pressure-test report, emission certificate, and operation instructions. Require a valve data book with serial-number traceability for body, trim, bellows, welds, and pressure tests. Define inspection and test plan hold points before production, including any required non-destructive examination.
Regulatory Compliance Market location, pressure equipment category, hazardous area, and plant safety rules. EU pressure equipment installations may fall under Directive 2014/68/EU, depending on fluid group, DN, and PS. Determine the applicable conformity-assessment route before ordering the valve. Confirm required marking, declaration, notified-body involvement, and documentation with the project authority.
Lifecycle and Maintenance Expected cycles, accessibility, spare parts, shutdown intervals, and total cost of ownership. Bellows reduce stem-emission risk but do not eliminate the need for correct installation and periodic inspection. Prefer a design with accessible packing, replaceable gaskets where practical, clear stem indication, and documented spare parts. Review cycle life, inspection intervals, bellows failure indication, and the manufacturer’s maintenance procedure.
Final Selection Gate All process, mechanical, safety, regulatory, and commercial requirements are complete. Select only after verification Approve the valve when DN, PN, materials, temperature, medium compatibility, leakage class, actuation, dimensions, and documents are confirmed. The final pressure-temperature envelope and material compatibility must be confirmed against the certified valve data sheet for the exact configuration.

Compare Materials, Pressure Ratings, Sizes, and End Connections

How to Choose DIN Bellows Sealed Gate Valves in 2026?

Material choice should follow the fluid, temperature, and corrosion risk. Carbon steel suits many steam and water services. Stainless steel, especially 316L, offers stronger protection against corrosive media. Bellows material needs equal care. 316L works widely, while nickel alloys may suit severe chemical exposure. Grand View Research’s 2024 industrial valve market assessment values the global market above US$75 billion in 2023. That scale reflects demand, not automatic quality. I would not trust a catalog number alone.

Pressure ratings require temperature checks. DIN PN16, PN25, and PN40 are not fixed limits in every service. EN 12516 pressure-temperature tables show allowable pressure decreasing as temperature rises. Size the valve from flow rate, line velocity, and pressure drop. An oversized DN100 valve on a small process line may control poorly. End connections also affect installation risk. EN 1092-1 flanges support common DIN piping layouts, while butt-weld ends reduce bolted joints and dead space. Check wall thickness, face dimensions, and field welding procedures.

Tips: Match the body and bellows materials with the process datasheet. Verify pressure ratings against operating temperature. Request leakage testing to EN 12266-1, and fugitive-emission classification under ISO 15848-1 when emissions matter. Confirm the actual pipe schedule before ordering. Small details are often missed.

Evaluate Bellows Performance, Sealing Reliability, and Safety Features

How to Choose DIN Bellows Sealed Gate Valves in 2026?

When evaluating a DIN bellows sealed gate valve, inspect the bellows before comparing prices. Its material must suit the fluid, temperature, pressure, and operating cycle. Stainless steel may perform well, but compatibility data still matters. Ask for tested cycle life, weld inspection records, and pressure-test results. A small weld defect can become a serious leak after repeated heating and cooling. Check the bellows stroke, forming method, and fatigue design. These details reveal more than a polished product sheet.

Sealing reliability depends on more than the bellows. Examine bonnet gaskets, stem guidance, body joints, and end-connection quality. A secondary seal can provide valuable protection if the bellows fails. Request helium or equivalent leak-testing data when the service is sensitive. Also confirm the stated leakage rate and test conditions. Numbers without test methods are weak evidence. They need context.

Safety features deserve practical attention. Look for a position indicator, secure handwheel, anti-ejection stem design, and a locking option where accidental operation matters. For trapped fluids, review cavity-pressure relief or thermal expansion protection. Confirm whether the valve supports remote leak monitoring. Installation space also affects safe maintenance. Measure the bonnet height and actuator clearance. One often-missed detail is drain access. It can complicate inspection later. No selection is perfect. A valve rated for extreme conditions may operate poorly if oversized, cycled rarely, or installed without proper alignment. Have an experienced engineer review the duty cycle, drawings, certificates, and maintenance plan before approval.

How to Choose DIN Bellows Sealed Gate Valves in 2026?

Evaluate bellows performance, sealing reliability, and safety features by first matching the valve’s nominal pressure class to the piping-system design pressure.

The chart shows standardized PN nominal pressure classes commonly used for EN/DIN-designated industrial valves: PN10, PN16, PN25, PN40, PN63, PN100, and PN160. PN values are reference pressure designations in bar at defined reference conditions; the allowable working pressure can decrease with temperature, material, and design limitations. Selection should also verify bellows-cycle qualification, body and bonnet pressure testing, seat leakage performance, overpressure protection, and applicable requirements such as EN 12266-1 and EN 12516.

Verify Standards, Installation Needs, Maintenance, and Supplier Quality

How to Choose DIN Bellows Sealed Gate Valves in 2026?

Choosing a DIN bellows sealed gate valve starts with the service conditions. Confirm the applicable DIN or EN standard, pressure class, temperature range, face-to-face dimension, and testing requirements.

EN 13709 may apply to industrial gate valves, while EN 12266 supports pressure testing verification. Do not rely on a catalogue title alone. Request material certificates, pressure test records, and a clear datasheet.

The bellows must match the medium, especially when handling corrosive, toxic, or high-temperature fluids.

Installation details often decide long-term performance. Check pipe alignment before bolting. Even small external stress can distort the valve body.

Follow the marked flow direction and installation position. Leave enough clearance for handwheel operation, insulation, and future bellows inspection.

During commissioning, operate the valve slowly and check for leakage around the bonnet, flange, and stem area. A perfect checklist can still miss poor site workmanship.

Tips: Ask the supplier for EN 10204 3.1 certificates, shell and seat test results, bellows cycle data, spare-part availability, and documented quality procedures. Confirm whether testing covers the actual pressure and temperature range. During maintenance, record operating cycles and torque changes. Inspect for corrosion, damaged packing, and abnormal movement. Do not treat a sealed bellows as permanent protection; repeated thermal cycling can shorten its life. Supplier responsiveness matters too. If technical answers arrive vague or late, reconsider the purchase before installation.